vip@mingyuforklift.com
+86-0535-2090977

Published: October 2, 2026
HTML Meta Description: Electric stacker planning for RFID-visible compact replenishment, inventory accuracy, micro-hubs, manufacturing kits and safe handoffs.
Keywords: electric stacker, RAIN RFID logistics, inventory accuracy, compact replenishment, micro fulfillment, manufacturing kitting, narrow aisle stacker, ZGFORKLIFT, MYZG, warehouse visibility
RAIN in Action 2026 is highlighting the connection between digital inventory records and physical warehouse reality. Electric stackers can support that connection in pharmacy distribution, apparel returns, spare-parts supermarkets and flexible manufacturing, where compact buffers and frequent scans must still respect load stability and human right-of-way.
Start with a documented task and route survey. Record the narrowest aisle and turn, doorway and gate width, overhead clearance, maximum gradient, dock edges and the worst surface condition. Measure real loads at their actual load centers, including long, offset or irregular items. Nameplate capacity is only a starting point; residual capacity at the required height and with the selected attachment determines practical application fit.
RFID can find a discrepancy quickly, but operations still need a controlled process to verify, isolate and move the affected pallet. The stacker route and buffer should make exceptions visible instead of burying them in overflow stock.
Review the CQDH20 electric reach stacker as the first product reference, then confirm current specifications with the manufacturer.
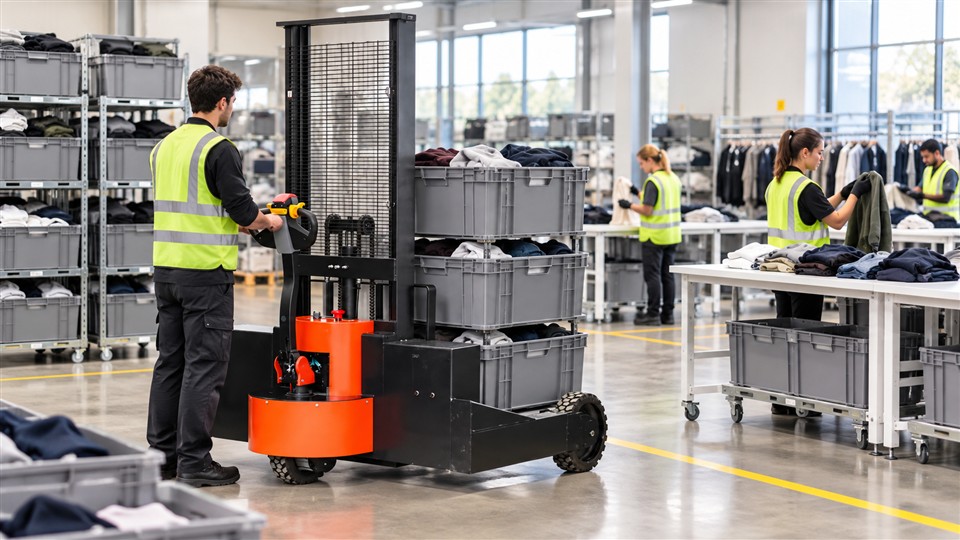
Match aisle width, turning radius, lift height, residual capacity, fork geometry, wheel material and battery endurance. Verify rack protection, scanner placement and every conveyor or cell handoff height.
Visibility and control deserve the same attention as capacity. Review the mast, carriage, tyres or wheels, lighting, mirrors or cameras, restraint, warning devices and speed management as one system. Dust, cold, heat, moisture and corrosion may require extra protection and shorter inspection intervals. Operators must see the travel path and place the load without leaving the protected operating position.
Compare the CDD15G electric walkie stacker for a second view of capacity, manoeuvrability, energy and service access.
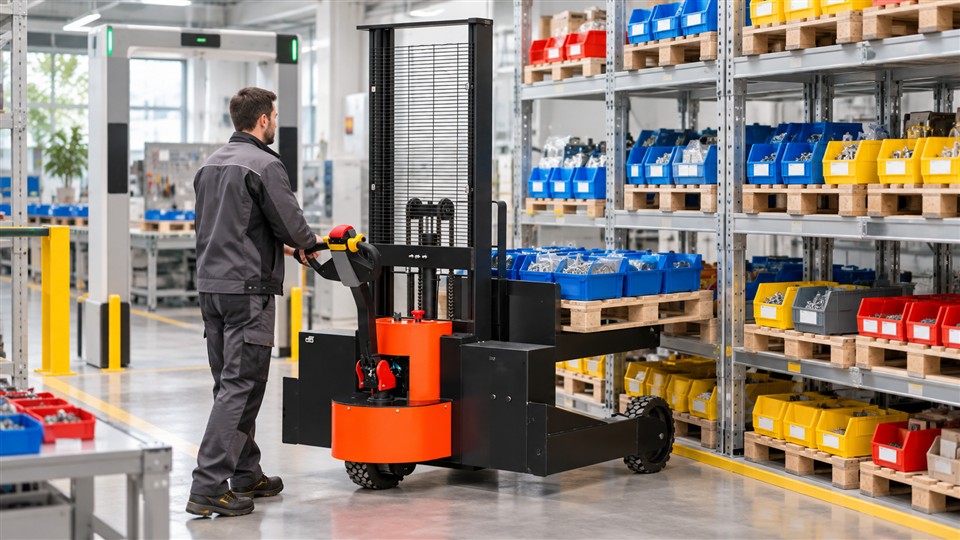
Separate manual stacker routes from mobile robots, protect scanning and handoff points, and never enter an automated cell until energy and movement are controlled under the approved procedure.
Create a written operating envelope for every approved route: maximum load and lift height, travel direction, pedestrian exclusion points, slope rules and stop-work conditions. Complete a pre-shift inspection of tyres or wheels, forks, chains, hoses, brakes, steering, alarms and the energy or fuel system. Isolate defects affecting stability, braking or visibility until corrected.
Supervisors should observe real work, record near misses, harsh braking, overload attempts, impacts and recurring service issues, then improve layout, traffic separation and coaching. Build the business case around productive hours rather than purchase price alone. Include operator time, maintenance, energy or fuel, infrastructure, transport, downtime risk and resale value.
The ZG-MYCPDB counterbalanced stacker is the third internal product reference for application comparison.
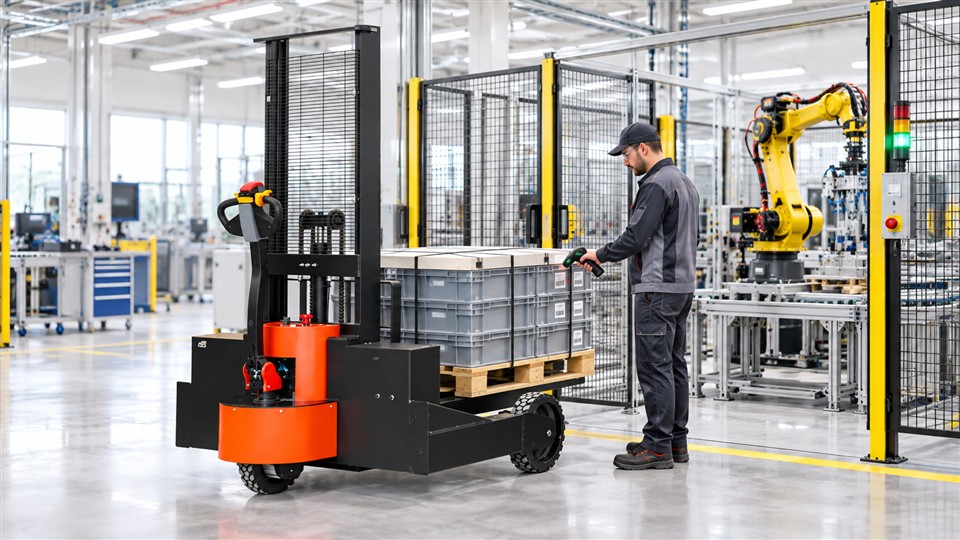
Track replenishment lead time, buffer occupancy, scan exceptions, manual searches, damage, battery use and line stoppage. Measure improvement during representative peak periods.
A staged trial is the strongest way to validate a configuration. Select a representative route, define success measures, brief operators and compare throughput, energy use, handling accuracy and maintenance observations. Review results with operations, safety and finance before fleet-wide deployment. This evidence turns a current industry headline into a defensible material-handling plan.
ZGFORKLIFT and MYZG can tailor the final specification after reviewing the application. Product availability varies by market; confirm the latest technical data and comply with local regulations before purchase or operation.
Contact Shandong Zhuogong Machinery equipment Co.,Ltd. Email: vip@mingyuforklift.com. Tel: +86-0535-2090977. WhatsApp: +86 131 8160 2336. Address: Xiaqiu Town, Laizhou, Yantai City, Shandong Province, China.
Send the maximum load, load-center distance, aisle width, gradient, surface condition, daily duty hours and climate so MYZG engineers can recommend a practical configuration instead of a generic catalogue answer.
Name: selena
Mobile:+86-13176910558
Tel:+86-0535-2090977
Whatsapp:8613181602336
Email:vip@mingyuforklift.com
Add:Xiaqiu Town, Laizhou, Yantai City, Shandong Province, China